


Cold Rolling Mill Machine Of The Operate Side Work Roller Bearing Block
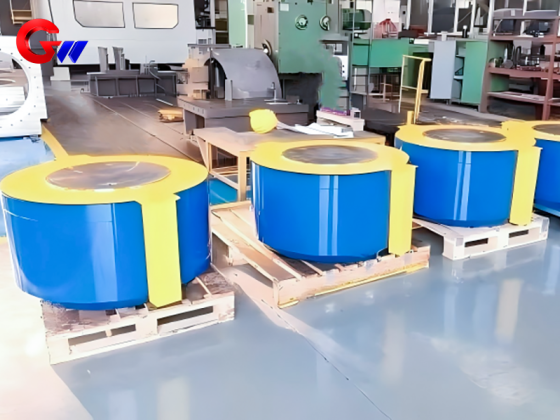
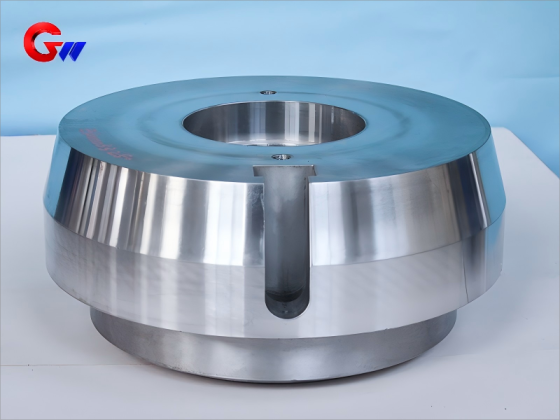
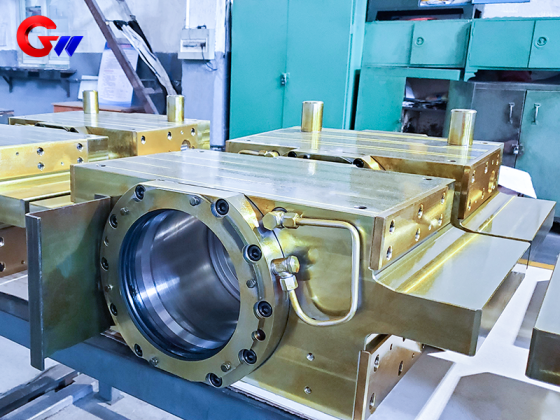
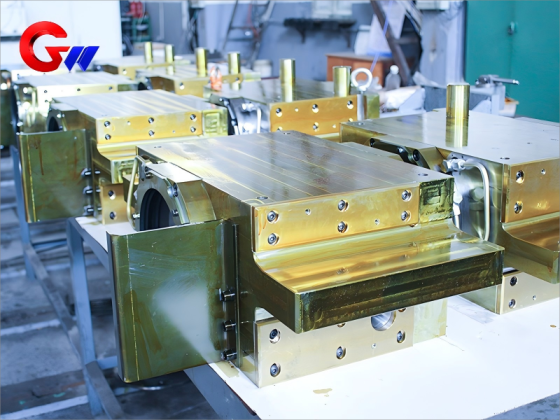
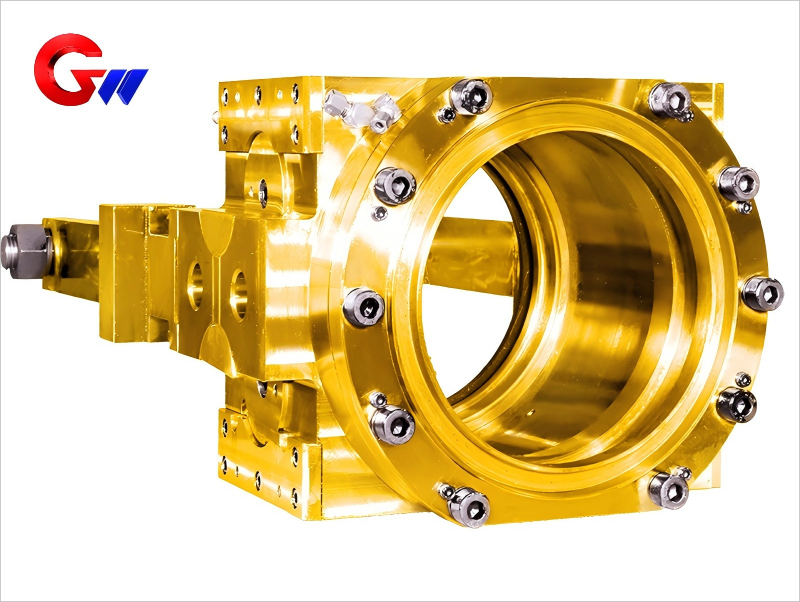
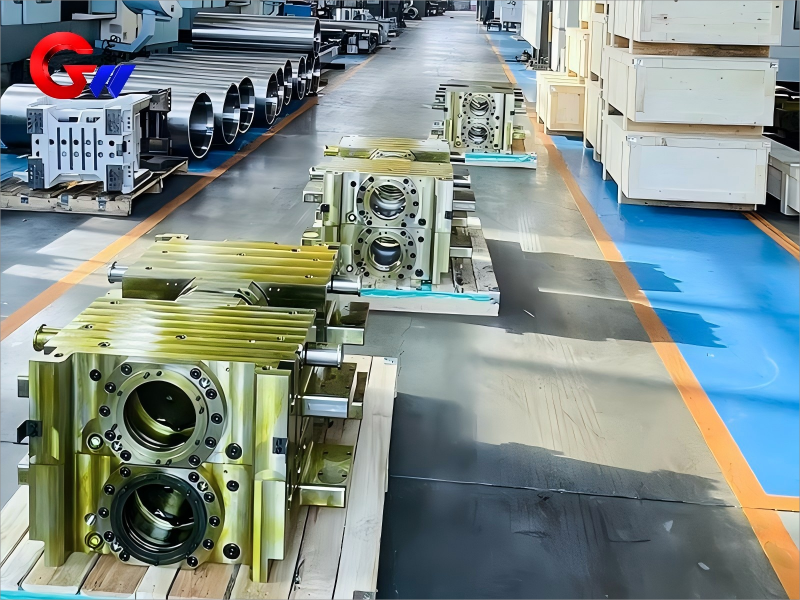
The operating-side work roll bearing block is a precision-machined support component designed for the work roll assembly of a cold rolling mill. It provides accurate bearing positioning, stable structural support, and reliable alignment for work roll operation under continuous rolling conditions.
Designed for stainless steel, silicon steel, and ultra-thin strip production, this component combines QT600-3 ductile iron construction, controlled heat treatment, precision CNC machining, high-accuracy bearing interfaces, oil-air lubrication, and multi-stage sealing.
Key Features
- High-precision positioning: Work roll radial runout controlled to ≤ 0.01 mm, supporting precision strip rolling.
- Efficient roll changing: Integrated hydraulic locking mechanism with a target roll change time of ≤ 10 minutes.
- Vibration control: Designed for high-frequency vibration control within 20–500 Hz, with specified amplitude of ≤ 0.5 μm.
- Precision bearing interface: Bearing hole cylindricity controlled to ≤ 0.003 mm.
- Multiple rolling mill applications: Suitable for six-high UC-MILL and twenty-high Sendzimir rolling mill configurations.
Brand: GW Precision
Product Origin: Luoyang, China
Delivery Time: According to contractual agreement
Supply Capacity: Up to 1,000 pieces per year
- GW Precision
- China,Luoyang
- Contractual Stipulation
- Anual Capacity is 1000 pieces
- Information
Cold Rolling Mill Machine Of The Operate Side Work Roller Bearing Block
Material and Heat Treatment Specification
Main Material
The work roll bearing block is manufactured from QT600-3 ductile iron, corresponding to EN-GJS-600-3. The material is selected for its combination of structural strength, dimensional stability, vibration damping, and suitable strength-to-weight characteristics.
The specified material density is approximately 7.1 g/cm³. Its mechanical and damping characteristics make it suitable for supporting the work roll and bearing assembly in a precision cold rolling mill.
Chemical Composition
| Element | Specification |
|---|---|
| Carbon (C) | 3.6–3.8% |
| Silicon (Si) | 2.2–2.5% |
| Manganese (Mn) | ≤ 0.3% |
| Magnesium (Mg) | 0.03–0.05% |
The material is designed to provide adequate structural rigidity while contributing to vibration attenuation during rolling. The specified vibration attenuation rate is ≥35%.
For an operating-side application, material stability is particularly important because the support structure must maintain the relative position of the work roll, bearing assembly, and hydraulic components during repeated rolling cycles.
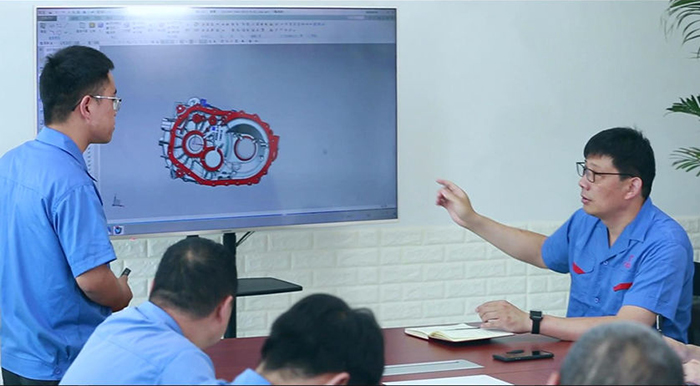
Key Component Materials and Surface Treatment
Different functional areas of the rolling mill bearing block use materials and surface treatments selected according to their operating conditions.
| Component | Material | Treatment |
|---|---|---|
| Bearing block body | QT600-3 ductile iron | Isothermal quenching and shot peening strengthening |
| Wear-resistant liner | GCr15SiMn | Deep cryogenic treatment + 20 μm hard chromium plating |
| Sealing component | PTFE + 316L | Laser micro-texturing |
The QT600-3 body forms the main structural section of the work roll bearing block. Isothermal quenching and shot peening are applied according to the specified manufacturing process.
The wear-resistant liner uses GCr15SiMn. Deep cryogenic treatment and hard chromium plating are used to improve the service characteristics of the liner, with a specified chromium plating thickness of 20 μm.
PTFE and 316L are used for the sealing components. Laser micro-texturing is applied to the specified sealing surfaces to support the required sealing and operating characteristics.
The combination of these materials allows the component to integrate structural support, wear resistance, and sealing functions within the same cold rolling mill assembly.
GW Precision Heat Treatment Process
Isothermal Quenching
The main body of the work roll bearing block undergoes a controlled heat treatment process:
Heating: 900°C × 2 h
Salt bath quenching: 300°C × 1 h
Air cooling
Dimensional Stability Treatment
Aging treatment: 180°C × 24 h
Specified dimensional change: ≤0.005%
Heat treatment is an important part of the manufacturing process because dimensional stability directly affects the accuracy of the bearing interface and installation surfaces.
For a precision rolling mill bearing block, uncontrolled dimensional changes after machining may influence bearing installation and the alignment relationship between the bearing, work roll, and mill structure. The specified aging treatment is therefore used to improve dimensional stability before final precision machining and inspection.
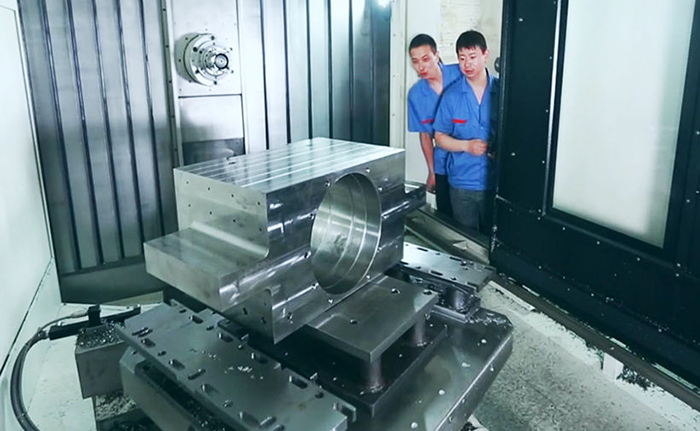
Mechanical Machining Accuracy
Dimensional accuracy is one of the key manufacturing requirements for the work roll bearing block. Critical bearing and mounting interfaces are inspected according to specified tolerance levels.
Critical Dimensional Tolerances
| Feature | Specification | Inspection Method |
|---|---|---|
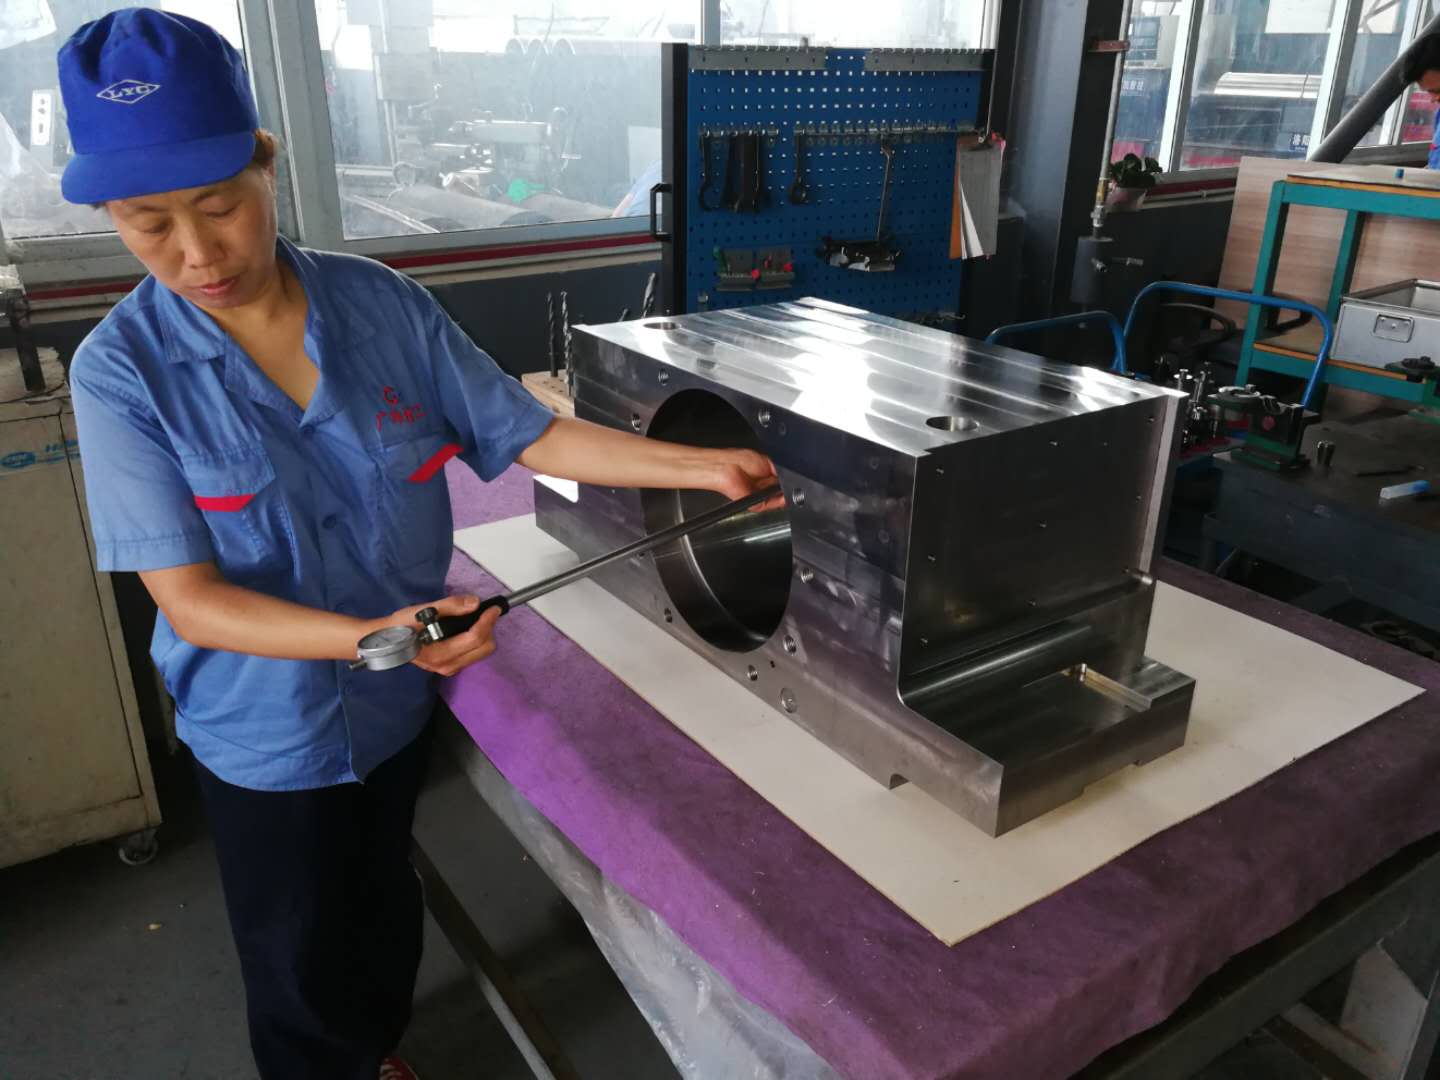
| Bearing hole | Φ200–400 mm, IT4 | Electronic plug gauge + roundness tester |
| Hydraulic cylinder installation surface | Flatness 0.01 mm | Optical flat |
| Positioning pin hole | H6 | Coordinate Measuring Machine |
| Bearing hole cylindricity | ≤0.003 mm | Precision dimensional inspection |
| Installation surface verticality | ≤0.005 mm/100 mm | Precision dimensional inspection |
The bearing hole is a critical interface between the work roll bearing assembly and the support structure. A cylindricity requirement of ≤0.003 mm is specified to maintain the required geometrical condition.
The hydraulic cylinder installation surface has a flatness requirement of 0.01 mm, while positioning pin holes are manufactured to H6 tolerance.
The verticality of each installation surface is controlled to ≤0.005 mm/100 mm. These controls help maintain the installation relationship of the component within the cold rolling mill.
Lubrication System
The work roll bearing block uses an oil-air lubrication system for controlled lubricant delivery to the bearing-related operating area.
Oil-Air Lubrication
Lubricant: ISO VG 68 synthetic ester oil containing MoS₂ additive
| Parameter | Specification |
|---|---|
| Oil volume | 0.05 ml/time |
| Air pressure | 0.4–0.6 MPa |
| Frequency | 2–5 Hz |
| Adjustment | Automatically adjusted according to rolling speed |
The oil-air system provides controlled lubrication during continuous operation. Lubrication frequency can be automatically adjusted according to the rolling speed, helping maintain a suitable lubrication condition under changing production conditions.
For the operating-side assembly, stable lubrication contributes to reliable operation of the bearing interface and supports the continuous working requirements of the cold rolling mill.
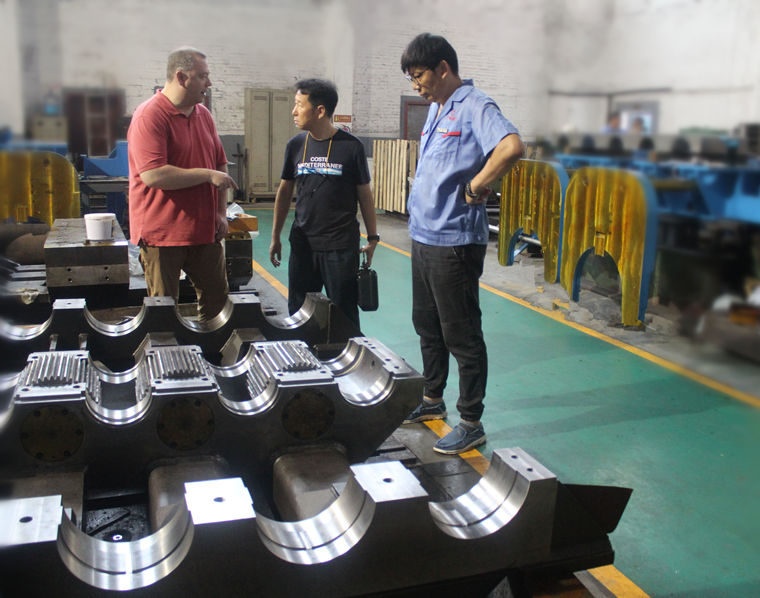
Application in Cold Rolling Mills
The operating-side work roll bearing block is designed for cold rolling equipment used in stainless steel, silicon steel, and ultra-thin strip production.
Six-High UC-MILL
The component can be applied to six-high UC-MILL configurations for stainless steel and silicon steel rolling.
Specified rolling thickness:
0.1–2.0 mm
The operating-side support arrangement provides the required interface for work roll positioning and bearing installation in this type of cold rolling mill.
Twenty-High Sendzimir Rolling Mill
The component can also be used for twenty-high Sendzimir rolling mill applications involving ultra-thin strip.
Specified rolling thickness:
0.02–0.2 mm
The precision requirements of ultra-thin strip production place particular importance on bearing alignment, dimensional stability, vibration control, and accurate positioning of the work roll.
Quality Control
GW Precision applies process-based quality control throughout the manufacturing of the work roll bearing block, including material preparation, heat treatment, CNC machining, precision inspection, cleaning, and final delivery.
Critical dimensions are inspected using appropriate measuring equipment, including electronic gauges, roundness inspection equipment, optical flat inspection, and coordinate measuring machines.
Particular attention is given to bearing holes, positioning holes, mounting surfaces, geometrical tolerances, and other functional interfaces.
The completed rolling mill bearing block is cleaned and deburred before final inspection. Inspection documentation is prepared according to the applicable production and contractual requirements.
Through controlled material selection, heat treatment, precision machining, dimensional inspection, lubrication design, and sealing configuration, GW Precision provides operating-side bearing support components for demanding cold rolling mill applications.
EMAIL:guangwei@gwspool.com